Line tooling · Auxiliaries · Henan Zhongsheng
Everything around the machine and the die.
A pultrusion line is more than the puller and the die. Creels, yarn drying ovens, resin baths, preform guides, winding units, mat cutters, cut-off saws and run-out tables decide whether the fiber arrives straight, wet and in the right place. Henan Zhongsheng builds this tooling for its own 26 lines and supplies it with a machine or on its own. pultrx, the factory’s export company in Shanghai, scopes it line by line in the quotation.
Where tooling sits in the chain
Specify tooling around the selected machine and die.
| Machine package to confirm | Haoli die table, puller, controls and cut-off scope; confirm each inclusion and tooling interface |
|---|---|
| Quoted as separate lines | Creels, yarn drying ovens, winding units, mat cutters, run-out tables, stackers, dust extraction, injection units |
| Supplied with the die | Preform guides and plates, trial parameters, first-sample record |
| Who builds it | Henan Zhongsheng Composite Material Co., Ltd., equipment workshop (since November 2022) and die shop (since August 2020) |
| Warranty party | Responsible legal entity confirmed separately for Zhongsheng tooling, Haoli machinery and any Huafan injection system |
| For lines by other makers | Stand-alone tooling supplied against photos and interface dimensions; preform guides need the die |
Eight tooling groups
What each piece does and what to tell us
Match each tooling group to your profile, reinforcement and line layout. Confirm ratings and interfaces in the quotation.
1 of 8
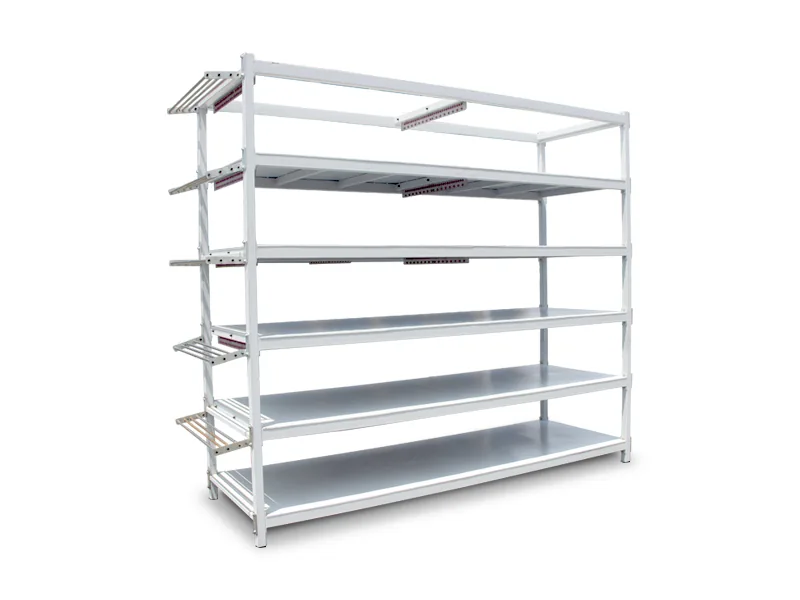
Creels
Hold the roving packages and let each end pay off at even tension so the fiber reaches the bath without twist or catenary.
What to specify
- Number of packages, package weight and inside or outside pull-off
- One guide eye per end, with wear-resistant bushings at the shelf ends
- Adjustable tension with a readable scale, so a setting can be repeated
- Separate mat and veil stands with height-adjustable mandrels on the process centerline
- Static-dissipative guide eyes if required, castors or fixed frame, and the route to the resin bath
2 of 8
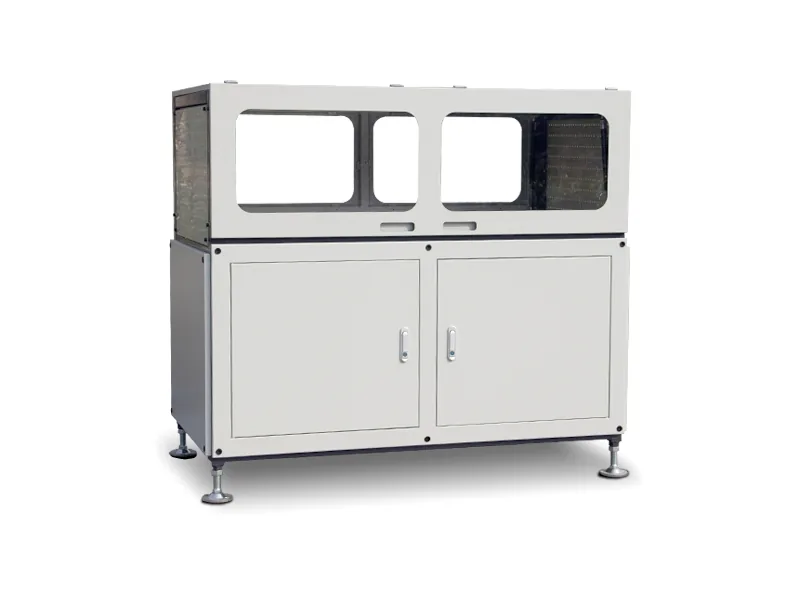
Yarn drying ovens
Condition roving before impregnation. The factory fits them on rebar and rock-bolt lines, where dry fiber gives even wet-out and a cleaner sand-coated surface.
What to specify
- Moisture limit for the fiber, from your resin supplier; polyurethane is the most sensitive
- Whether the resin system needs preheated fiber
- Temperature range and the number of ends passing through
- Position between creel and bath
3 of 8
Resin baths and impregnation stations
Wet the reinforcement in an open bath before the die. A dip bath uses breaker bars to spread the fiber; a straight-through drip bath suits hollow and complex sections. Closed injection is covered under injection boxes below.
What to specify
- Resin system: polyester, vinyl ester, epoxy or phenolic
- Dip bath with breaker bars, or straight-through drip bath for hollow sections
- Bath volume, preheating, squeeze rollers, resin pump and solvent cleaning
- Bath table height adjustment and the drip tray up to the die entry
4 of 8
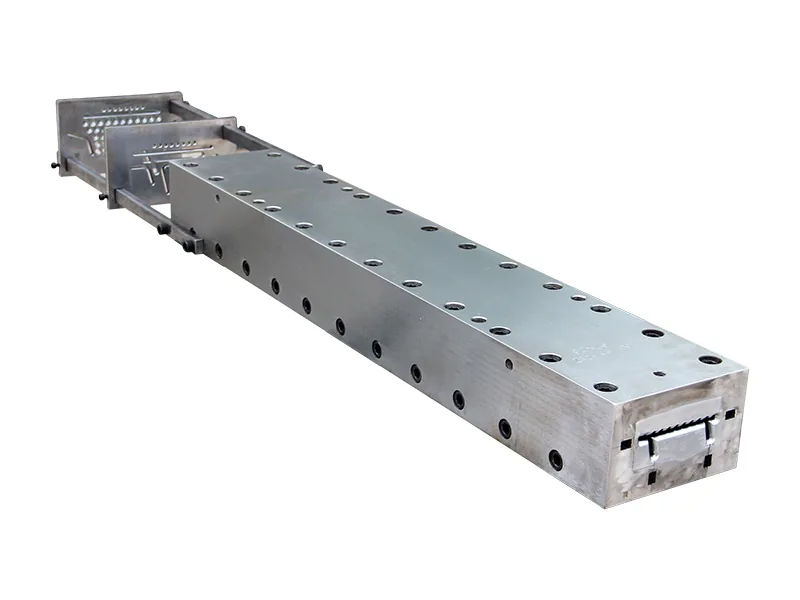
Preform guides and plates
Arrange rovings, mats and veils into the shape of the cavity before the die entry. They are designed with the die and trialed with it, which is why the die shop supplies them.
What to specify
- Reinforcement schedule: roving count, mats, multiaxial fabrics, veils, inserts
- Roving guide plates, mat and fabric formers, puller pads and saw guides listed as one set per die
- Material of the plates and how they mount on the die table
- Spare sets for a second resin system or a surface veil
5 of 8
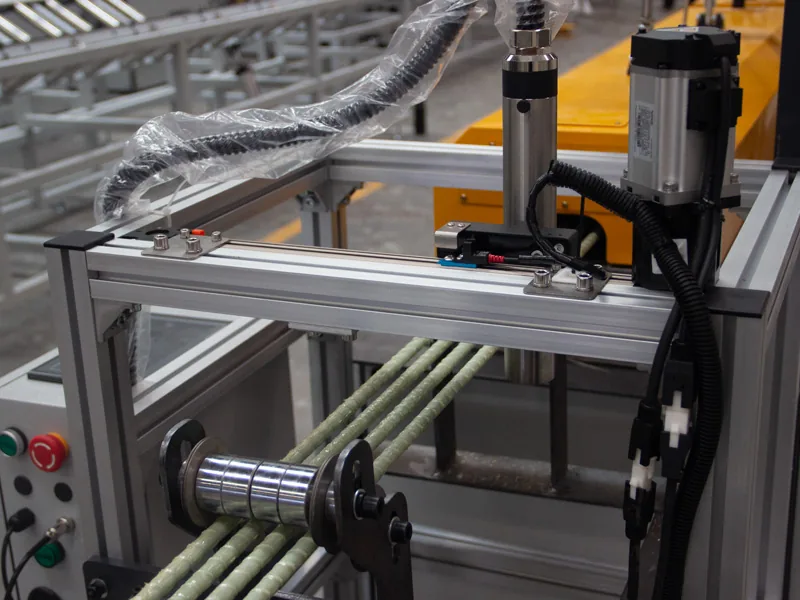
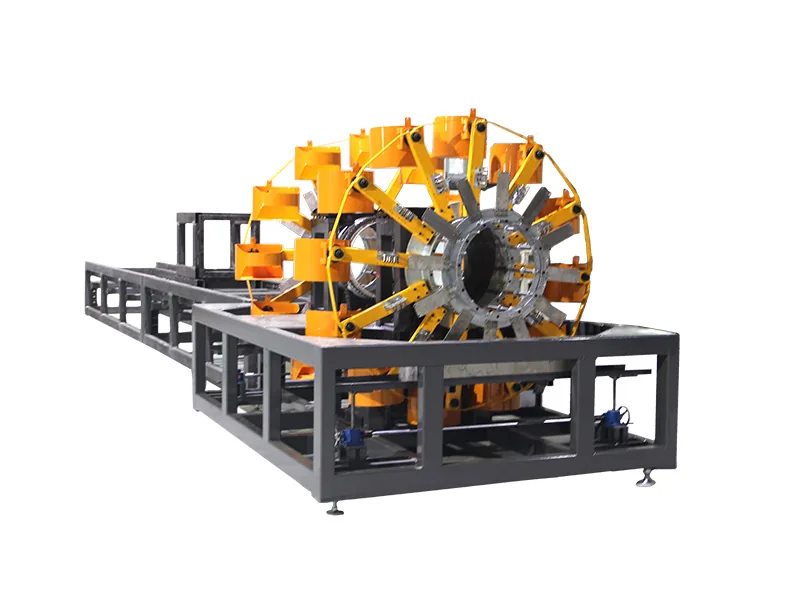
Winding units
Wrap hoop or helical fiber onto the pulled core for wound-and-pultruded tubes, rods and rock bolts. Winding speed follows the line speed so the wrap angle stays constant.
What to specify
- Product: tube, rod or rock bolt, and the wrap angle or rib pitch
- Number of spools and spool size
- Whether the unit is part of a new line or retrofitted to an existing puller
6 of 8
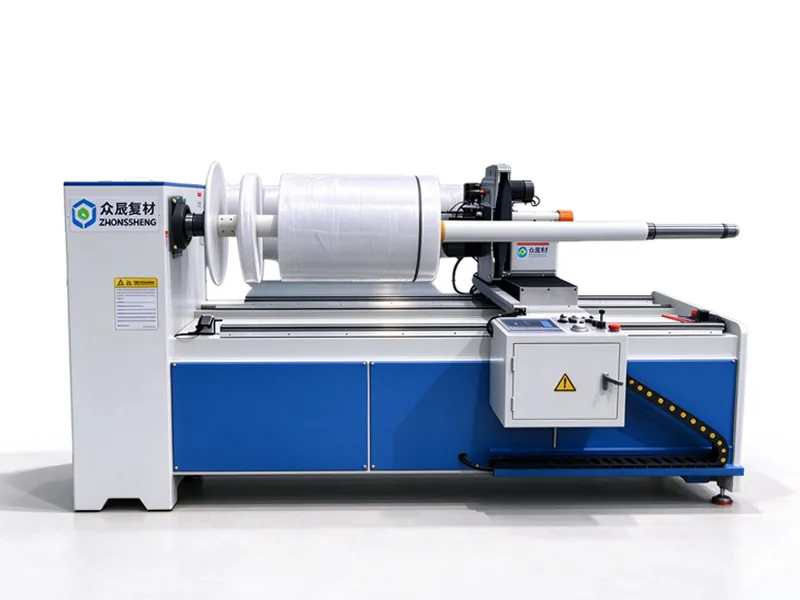
Mat and veil cutting machines
Slit mat, veil and fabric rolls into the strip widths the preform needs. Adjustable speed and an optional tensioner keep the strip edges straight.
What to specify
- Roll width, roll diameter and core diameter of the mat you buy
- Strip widths, number of knives and a preset cut count
- Cutting speed, width readout, tension control and rewind
7 of 8
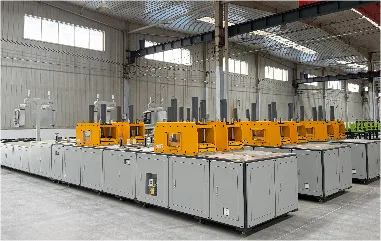
Cut-off saws and run-out tables
Cut the moving profile to length without stopping the line and carry the lengths away. Flying saws are supplied with the machine; run-out tables, stackers and dust extraction are scoped with the layout.
What to specify
- Flying saw that clamps the profile and travels at line speed, or a dead-stop saw on a moving table
- Cut length set by encoder, and the length tolerance
- Blade type and dust extraction for the resin and fiber
- Run-out length, flippers or stacking bin, and the interlock with the puller
8 of 8
Closed injection boxes and metering units
Replace the open bath with a sealed box at the die entry, fed by a two-component metering unit. Polyurethane needs it to keep air moisture out of the resin, and two-component epoxy can use the same route. The factory lists its own metering unit for the polyurethane lines it runs; the Huafan YH-2700 is the separately supplied system on this site. Your quotation names which unit is offered and who the warranty party is.
What to specify
- Resin and hardener or isocyanate ratio, output and pressure
- Injection box material, length and how it joins the die
- Heating, vacuum feed and automatic flushing
- Puller rating for the resin: builders report higher pull force for polyurethane than for polyester
Beyond the eight groups
More line items buyers specify
International machine and tooling makers list these items in their own scopes. Decide early whether your product needs them, because each one changes the layout and the acceptance trial.
| Item | What it does | What to specify | In a pultrx quotation |
|---|---|---|---|
| Die heating platens and zones | Heat the die in independent zones. Long or thick dies, and polyurethane dies, need more zones. | Number of zones, platen length, controller type, entry and exit cooling | Heating and controllers come with the machine; the zone layout is set with the die |
| Radio-frequency preheaters | Warm thick rods, tubes and rebar bundles before the die so the core cures with the skin. | Frequency, power, electrode arrangement, temperature readout and alarms | Not built by the factory. If you buy one, the layout reserves the space and the puller interlock |
| Cooling after the die | Cool the profile before the saw and before coiling or stacking. | Water bath or air, length, water supply and drainage | Quoted with the run-out where the product needs it, for example on rebar lines |
| Coilers and stackers | Coil small rods and bars, or stack and bundle cut lengths. | Bar diameter, coil size, stack height and bundling | Scoped with the layout and the product mix |
| Process monitoring and data | Record pull force, line speed and die temperatures, and show trends to the operator. | Signals logged, storage period, export format, alarms and remote access | Through the machine PLC and HMI as quoted. In-die cure sensors are third-party items |
| Resin mixing room | Weigh, mix and transfer resin, filler and catalyst to the line. | Batch size, mixer, scales, catalyst dispenser, filler storage, transfer pumps, solvent recovery, ventilation | Scoped in a turnkey line quotation; your building and ventilation stay with you |
Global benchmark
What international tooling makers publish
Use these published figures to write your own tooling RFQ. They describe each maker's equipment, not the factory's; the quotation states the ratings of the tooling we supply.
| Group | Published figure | Source |
|---|---|---|
| Creels | Roving creels for packages of 40 lb or more, 48 or 100 positions; mat creels for rolls up to 610 mm diameter with height-adjustable mandrels | Strongwell PULSTAR |
| Creels | One set of guide eyes per roving; tension from interlocking polished rods with a scale and locknut | Pultrex |
| Dies | High-alloy steel dies about 0.75 to 1.5 m long, often polished and chrome plated | European Pultrusion Technology Association |
| Dies | Die lengths typically 61 to 122 cm, hard chrome plating and ion nitriding | Strongwell PULSTAR |
| Dies | Dies up to 2,000 mm long with or without injection, ground chrome up to 100 µm, mandrels up to 6,000 mm | LUM Industry |
| Die heating | 2 to 8 self-tuning heating zones as standard, up to 24 as an option | Pultrex / KraussMaffei |
| Injection | Injection box about 50 cm long building pressure up to 100 bar; curing die with three heating zones; up to 3 m/min | KraussMaffei iPul |
| Injection | Closed impregnation for polyurethane; die about 1 m with 3 to 6 heating zones up to 230 °C | Covestro |
| Preheating | Multi-electrode radio-frequency preheaters at a nominal 80 MHz for rods, tubes, rebar and insulators | Thermex-Thermatron |
| Slitters | Rolls up to 620 mm wide and 2,000 mm diameter on 76 or 102 mm cores, 0 to 75 rpm, digital width readout | Pultrex |
| Cut-off | Flying saw with the profile clamped to a table moving at line speed; encoder-set cut length; dead-stop and dual-cut options | Strongwell PULSTAR |
| Monitoring | In-line pull-force transducers with trend displays for pull speed and force | Strongwell PULSTAR |
| Monitoring | In-die sensor for resin arrival and cure, rated to 100 bar and 210 °C, with a Pt100 temperature element | Synthesites |
For the machines themselves, see pultrusion machine manufacturers compared.
Scope
Covered and not covered
In a tooling quotation
- Each item as a separate line with its rating and interface
- Preform guides matched to the quoted die and reinforcement schedule
- Layout drawing showing where each item stands
- FAT of tooling together with the machine where ordered together
- Spare knives, rollers and guide eyes as listed
Agreed separately
- Raw materials for trials beyond the first sample
- Civil work, utilities and dust extraction ducting at your site
- Injection units from Huafan, quoted under that supplier’s scope
- Retrofit engineering on a line we did not build, quoted after photos and measurements
- Local electrical conformity assessment at destination
Questions buyers ask
Tooling questions
- Is line tooling included in the machine price?
- The agreed machine configuration determines what is included. Confirm the die table, puller, controls and cut-off package with Haoli. Creels, yarn ovens, baths, preform guides, winding units, mat cutters, run-out tables and injection units are listed as separate lines in the quotation so you can see what is included and what is not.
- Can I buy tooling for a line from another maker?
- Yes. Creels, ovens, winding units and mat cutters are stand-alone machines. Preform guides are made to a die, so the factory needs that die drawing or the die itself. Send the make and model of the existing line and photos of the interfaces.
- Who designs the preform guides?
- The die shop, together with the die. The preform set is trialed with the die on the factory’s own line and ships with the start-up parameters from that trial.
- Do you supply the resin injection system for polyurethane?
- Two routes. The factory lists its own metering and injection unit for the polyurethane lines it operates. pultrx also lists the Huafan YH-2700 system under a separate supplier category. The quotation states which one is offered, the responsible legal entity and the warranty party.
- How does this tooling compare with what European and US makers publish?
- The reference table on this page lists what Pultrex, Strongwell, LUM Industry, KraussMaffei, Covestro and Thermex-Thermatron publish for creels, dies, heating, injection, preheating and cut-off. Use those fields in your RFQ. The factory confirms each rating for its own tooling in the quotation; a published figure from another maker is not a specification of ours.
- What tooling does a GFRP rebar line need?
- Creel, yarn drying oven, resin bath with squeeze rollers, helical winding unit, sand-coating station if specified, curing oven, water cooling, caterpillar haul-off, flying saw and a coiler for small diameters. These are process items to review for the intended bar geometry; availability and the supplied stations require a project-specific equipment proposal.
Put this into a project record
Related worksheets & visual references
- Pultrusion Line Interface Map
Download a pultrusion line interface map and responsibility table for creels, resin impregnation, preforming, heated dies, pulling and cut-off.
Send the drawing. Get the tooling list in the right order.
Henan Zhongsheng tooling and dies are scoped through the Shanghai office. Confirm interfaces with Haoli machinery and any separate injection subsystem in the quotation.