Use this reference for your project
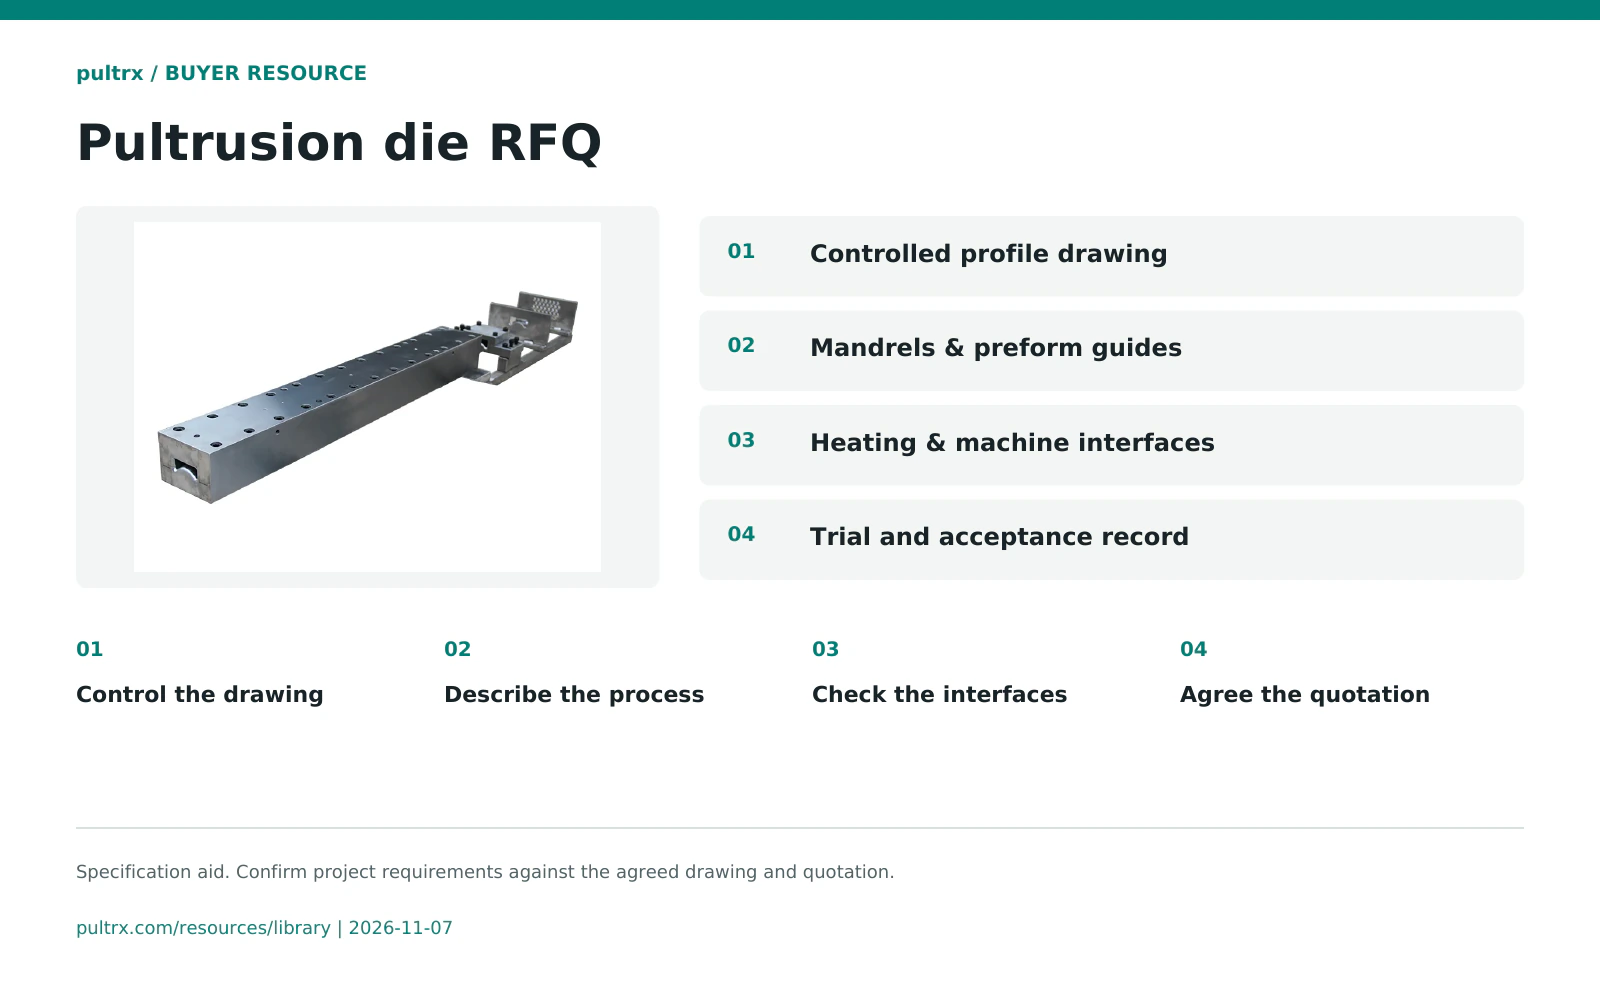
Use this pultrusion die RFQ worksheet to assemble a comparable tooling enquiry. The drawing package connects the finished profile to the die, mandrels, preform guides, heating arrangement and receiving line.
Separate the finished-profile requirements from proposed tool construction. Ask the supplier to identify deviations and exclusions before comparing quotations for a die, also called a mould.
How to use it
- 01
Control the drawing
Issue the profile section, units, revision, critical features and finished-part requirements.
- 02
Describe the process
State the resin, reinforcement arrangement, cavity count and intended trial material.
- 03
Check the interfaces
Record mounting, die envelope, heaters, sensors, preformers and line connections.
- 04
Agree the quotation
Itemize tooling, trials, acceptance records, ownership and post-delivery support.
Worksheet reference
Use these fields and checks with your project documents. Record the agreed values and evidence in the editable file.
| Package item | Buyer input | Supplier response to obtain | Document reference |
|---|---|---|---|
| Profile drawing | Revision, section, units and critical dimensions | Feasibility and proposed drawing departures | |
| Material package | Resin, reinforcement and formulation references | Compatibility and information needed for the trial | |
| Cavity and core layout | Required strands and hollow-section details | Cavity arrangement, mandrels and related tooling | |
| Receiving line | Die envelope, mounting and pulling arrangement | Mechanical interfaces and any line changes | |
| Heating and sensing | Available heaters, control zones and sensor interfaces | Included heaters, sensors and control responsibilities | |
| Preforming and impregnation | Fiber path and selected wet-out or injection route | Preform guides and resin-interface scope | |
| Trial and acceptance | Trial material, sample measurements and witness needs | Trial scope, records and acceptance method | |
| Commercial scope | Delivery, spares and tooling ownership requirements | Itemized price basis, exclusions and agreed responsibilities |
Scope and reading notes
- No default die length, temperature, line speed or material shrinkage allowance is specified. The supplier must review the actual process and profile.
- Keep preform guides with the die scope and identify any separately supplied heaters, controls or injection hardware.
- Tool acceptance and sample inspection do not establish finished-product conformity. Agree product qualification separately.
Sources and supporting references
Prepared by pultrx from the references below. Follow the linked product or guide for the full scope and source conditions.