Pultrusion die
Custom pultrusion die
A custom pultrusion die is designed from your cross-section drawing rather than taken from a catalogue family. The work starts with a design-for-manufacture review of wall thickness, radii and fiber layout, moves to a 3D model you approve, and ends with a trial pull on the factory's own line and a dimensional report before the die ships.
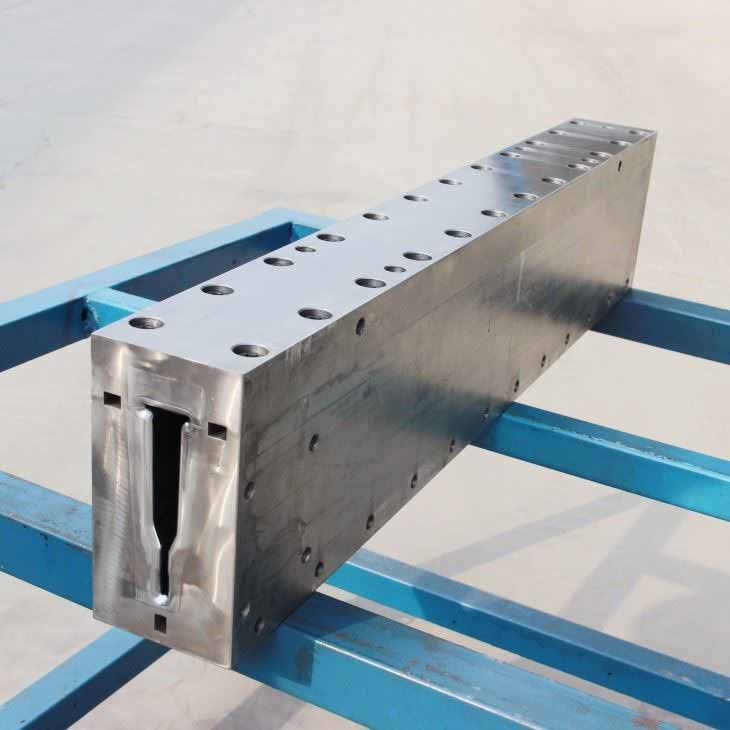
Specification
Configuration table
Every cell is either a figure supplied by the factory or TBD · ask factory. No typical values. Source: frpzs.com pultrusion die (mould) catalogue pages, fetched 2026-10-19; values are catalogue statements confirmed per die on the drawing.
| Parameter | Value |
|---|---|
| Die steel options | 40Cr, P20, Cr12MoV, 38CrMoAl or H13 (by application) |
| Base hardness | HRC 55–60 (catalogue) |
| Cavity surface treatment | Quench and temper, nitriding or induction hardening, hard chrome plating |
| Hard chrome thickness | 0.04–0.05 mm (catalogue) |
| Straightness | ≤ 0.02 mm over 1,000 mm (catalogue) |
| Profile dimensional tolerance | ±0.1 to ±0.3 mm depending on section (catalogue) |
| Resin systems | UP polyester, vinyl ester, epoxy, phenolic, polyurethane |
| Service life before re-chrome (m) | TBD · ask factory |
| Lead time (working days) | TBD · ask factory |
Scope of supply
What is included, what is quoted separately
Use these lists to compare scope. The signed quotation confirms the final inclusions and options.
Included in the base quotation
- DFM review of your cross-section and fiber layout
- 3D die model for your approval before steel is cut
- Machined, heat-treated and chrome-plated die with heating-plate interface
- Preforming guides for the profile
- Trial pull on the factory's own line with dimensional report and samples
Quoted separately on request
- Heating plates and thermocouples if your machine lacks them
- Mandrels and mandrel supports for hollow profiles (listed per die)
- Re-chroming and refurbishment of worn dies
- Resin injection box (for closed injection instead of an open bath)
- Shipping of trial samples by air
Cross-sections
Profiles covered by this die family
- Window and door frame sections
- Shutter and louver slats
- Ladder rails
- Cable ladder side rails
- Radome and antenna profiles
- Dies for third-party machines
Process
From drawing to die
What you supply and what you receive at each step.
- 01
Cross-section review
Buyer + die engineer
You send the drawing, resin system and target speed. The team checks wall thickness, radii and corners for pultrudability.
- 02
DFM feedback
Die engineer
Written feedback on changes that improve cure, fiber placement and die life, with the proposed fiber layout.
- 03
3D model approval
Buyer approval
Die plates, mandrel, heating layout and guide plates are modeled. Steel is cut only after you approve.
- 04
Machining and chrome
Die shop
Gantry milling, CNC, EDM and wire-cut, heat treatment, polishing and hard chrome plating.
- 05
Trial pull and report
Factory QC
The die runs on the factory's own line. You receive samples and a dimensional report before shipment.
From the workshop
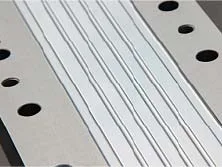
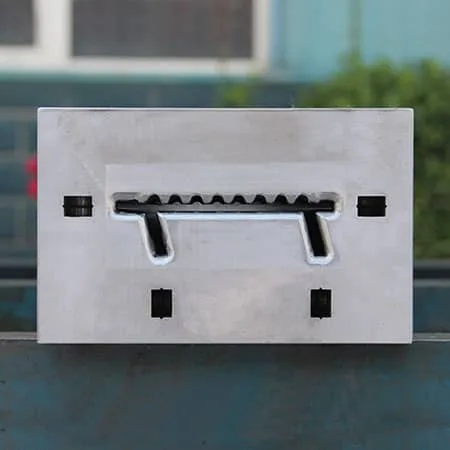
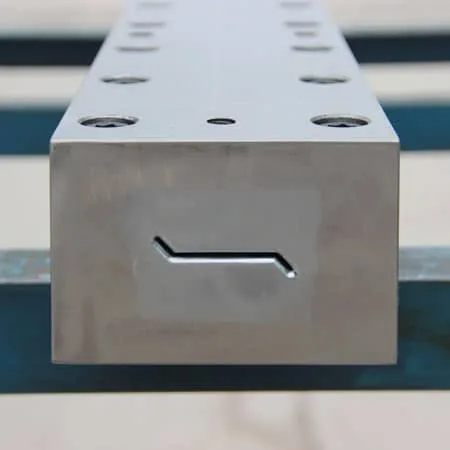
Photographs
Commercial terms
Who you contract with
- Manufacturer
- Henan Zhongsheng Composite Material Co., Ltd.
- Warranty party and term
- Henan Zhongsheng Composite Material Co., Ltd.; term and coverage confirmed in the written quotation.
- Contracting party and exporter of record
- Pultruded Export, Shanghai, China
- Incoterms
- FOB Chinese port by default; CIF/DAP on request
- Payment
- Milestones tied to drawing approval, FAT acceptance and shipment. Exact split on the quotation.
- Third-party inspection
- SGS, BV or TÜV pre-shipment inspection accepted, cost borne by the buyer
- Electrical
- 380 V 50 Hz standard; 480 V 60 Hz and other supplies on request. Destination electrical and conformity requirements must be agreed in the quotation; certification is not implied.
FAQ
Questions buyers ask
- What do I need to send?
- A DWG, STEP or PDF of the section, resin system, reinforcement schedule if known, tolerance requirement, target line speed and the machine the die will run on.
- Do I get samples before the die ships?
- Yes. A trial pull on the factory's own line produces samples and a dimensional report. Air freight of samples is quoted separately.
- Who owns the die design?
- Ownership of the drawing and die is set in the quotation. By default the buyer owns the die it pays for.
- Can you rework a die made elsewhere?
- Re-chroming and refurbishment of third-party dies is possible after inspection. Cracked or heavily worn cavities may need a new die.
Send a cross-section drawing. Get a scoped quotation.
Every quotation names the manufacturer, the exporter of record and the warranty party, and lists what is included.